For structural steel fabricators cutting 6–25 mm plate, the CNC plasma table has been the default workhorse for decades. It is fast enough, forgiving enough on rusty plate, and cheap enough to run that most shops never run the full lifecycle numbers on what happens after the cut: the grinding, the dross removal, the consumable churn, and the scrap rate.
That calculation has changed. High-power fiber lasers at 12–20 kW now cut the same thickness range at speeds that close the gap with HD plasma, while delivering edges that go directly to weld without secondary processing. For engineering specifications on structural plate processing, review our analysis of thick carbon steel cutting in heavy structural fabrication and our detailed breakdown of fiber laser vs high-definition plasma operating costs and edge taper. This guide compares a cnc plasma cutting table against a modern high-power fiber laser cell on cut edge perpendicularity, secondary labor, consumables, and full 5-year TCO.
Ⅰ. The Structural Shift: High-Power Fiber Laser Displacing Heavy Plasma Tables
1. Thermal column divergence vs. coherent focused beam physics
A plasma torch cuts by melting metal with an electrically conductive arc and blowing the molten material out with high-velocity gas. The arc column is wide, thermally diffuse, and produces a cut edge with a characteristic 3°–7° bevel. The heat-affected zone extends 0.5–1.5 mm into the material on each side.
A fiber laser focuses coherent light into a spot measured in fractions of a millimeter. The cut is narrow, the heat input is concentrated, and the edge is perpendicular within ISO 9013 tolerance without secondary processing. At the same thickness, the fiber cut produces less than half the HAZ depth of the plasma cut.
2. Piercing dynamics and speed crossover in 6mm–25mm structural steel
On 6–12 mm plate, a 12 kW fiber laser cuts at 3–5× the speed of a 200A HD plasma table. The gap narrows at 16–20 mm, where plasma retains an advantage in setup time on heavily scaled or rusty plate. By 25 mm, the comparison depends on power: a 20 kW fiber unit is competitive on speed, but a 400A HD plasma can still be faster on raw pierce time.
The economic decision at 20–25 mm is not about raw speed. It is about whether the edge quality eliminates downstream grinding and whether the nesting yield advantage justifies the capital premium.
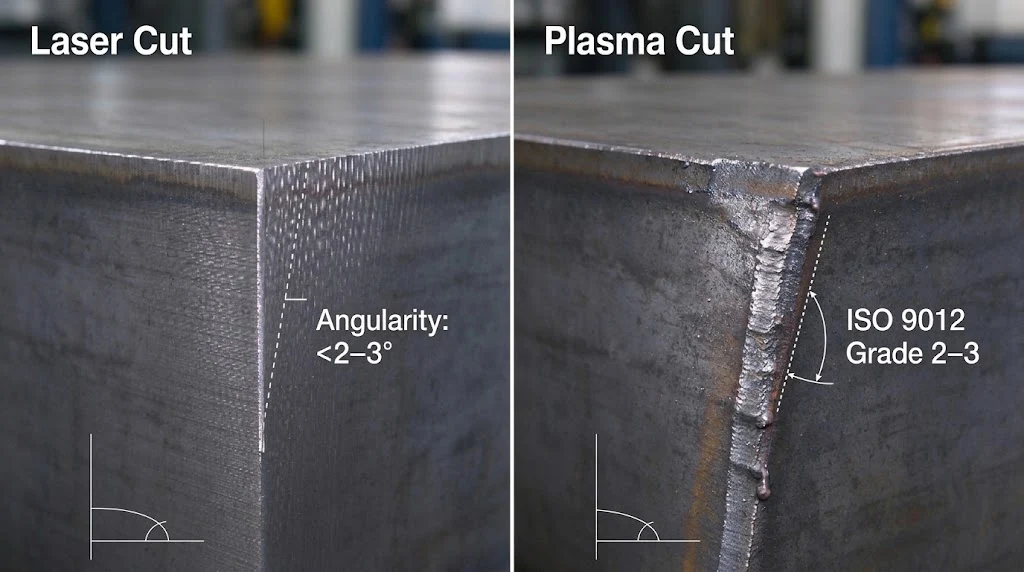
Table 1: Cut Edge Tolerances & Taper Comparison: Fiber Laser vs. HD Plasma
| پارامتر | Fiber Laser (12–20 kW) | HD Plasma (200–400A) | Practical Impact |
| Taper angle | ≤ 1° (ISO 9013 Range 1–2) | 3°–7° | Plasma requires larger weld gaps |
| Kerf width (16 mm) | 0.4–0.6 mm | 2.5–4.0 mm | Narrower kerf improves nesting yield |
| Minimum hole diameter | ~1× thickness | ~1.5× thickness | Laser cuts smaller bolt holes directly |
| HAZ depth | 0.1–0.3 mm | ۰.۵–۱.۵ میلیمتر | Plasma edge may require machining before weld |
| Surface roughness | Ra ≤ 12.5 μm | Ra ≤ 25 μm | Plasma shows visible drag lines |
Ⅱ. Cut Quality & Edge Taper: Eliminating the Secondary Grinding Bottleneck
The primary hidden overhead of operating a standard cnc plasma cutting table does not appear on the cutting cycle timer; it surfaces on the shop floor between blanking and assembly.
1. The root causes of plasma bottom dross: Remelted slag chemistry
Plasma cutting produces bottom dross when the high-velocity gas jet fails to fully eject the molten metal before it solidifies on the exit edge. The dross is a mixture of remelted steel and oxidized slag that adheres tightly to the cut face. Removing it requires a grinder, a chipping hammer, or a deburring station.
On 16 mm plate, typical dross removal time runs 1.2–1.6 man-hours per ton. For a shop cutting 120 tons per month, that is 144–192 man-hours of grinding labor per month—before counting the handling time to move parts to the grinding station and back.
2. Cut flank angularity and fit-up consequences
The 3°–7° bevel on a plasma cut edge has a downstream cost in weld fit-up. A T-joint or butt joint cut on plasma leaves a gap at the root that requires either a larger weld bead, a backup plate, or additional fitter time to close. On structural assemblies where the drawing specifies a tight root gap, plasma edges often require pre-weld grinding to remove the bevel.
Fiber laser cuts at ISO 9013 Range 1–2 perpendicularity. The edge is square enough to serve as the weld land directly, eliminating the fitter time and the grinding step.
3. Direct-to-weld part flow: Eliminating 1.2–1.8 man-hours per ton
When plasma dross and bevel are eliminated, the part flow changes. Parts come off the table and go directly to fit-up or to the welding station, with no grinding stop in between. The labor that was spent on deburring is redeployed or eliminated.
The table below quantifies that savings on a 120-ton-per-month structural fabrication baseline.

Table 2: Secondary Operations Elimination: Labor Cost Savings Ledger
| متریک | Plasma Table | لیزر فیبری | Delta |
| Deburring labor per ton | 1.4 hours | 0.1 hours | −1.3 hours/ton |
| Monthly volume (structural steel) | 120 tons | 120 tons | — |
| Monthly deburring labor hours | 168 hours | 12 hours | −156 hours |
| Fully loaded labor rate | $32/hour | $32/hour | — |
| Annual deburring labor cost | $64,512 | $4,608 | −$59,904 |
| Additional savings (handling, wheel wear) | — | — | ~$8,000/year |
Ⅲ. Consumables & Duty Cycle: Nozzles & Optics vs. Plasma Electrodes & Swirl Rings
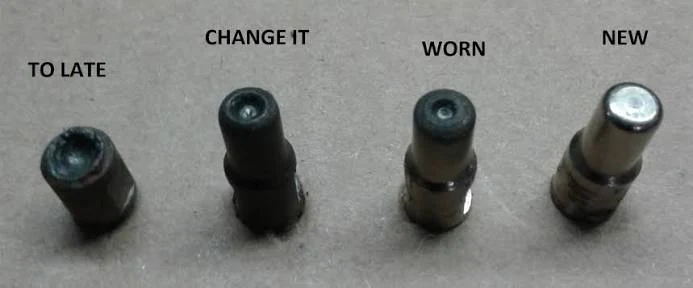
1. Plasma torch consumable erosion: Hafnium crater wear and arc wandering
The plasma electrode uses a hafnium insert that erodes with each arc start. As the crater deepens, the arc root wanders, and the cut quality degrades over the life of the consumable. A typical 200A electrode lasts 800–1,500 pierces; a 400A electrode lasts 400–800 pierces.
At 120 tons per month on 16 mm plate, that is 200–400 electrode changes per year, plus swirl ring and nozzle replacements. Each change is a 5–10 minute production stop, and the degraded cut quality near end-of-life produces scrap and rework.
2. Fiber laser optical delivery stability: Sealed solid-state protection
A fiber laser has no electrode to erode. The cutting nozzle is a passive gas orifice with a service life measured in weeks, not hours. The only optical consumable is the protective window at the cutting head, which is swapped in minutes when contaminated.
When a shop replaces a cnc plasma cutting table with a fiber cell, the consumable budget shifts from high-frequency electrode and nozzle churn to low-frequency window and nozzle replacement. That is a structural change in both cost and downtime.
3. Environmental and machine hygiene: Sludge disposal vs. dry downdraft
A plasma water table accumulates metal sludge that requires periodic dredging and disposal as regulated waste. The water itself needs treatment and replacement. The shop floor around the table is wet, and the cut parts require drying before the next process.
A fiber laser with dry downdraft extraction produces dry dust captured in a filter unit. There is no water table to maintain, no sludge to dispose of, and no wet parts to dry. The environmental compliance burden drops significantly.
Table 3: Consumables & Auxiliary Utility Consumption Ledger (Per 100 Meters of 16mm Steel)
| Cost Category | Fiber Laser (12 kW) | HD Plasma (200A) | Delta |
| Electrode/consumable cost | $0 | $18–$25 | −$20 |
| Nozzle / protective window | $4–$6 | $3–$5 | ~$0 |
| Assist gas cost | $6–$9 (O₂) | $10–$15 (O₂/N₂) | −$5 |
| Electricity (wall-plug) | $8–$11 | $14–$18 | −$6 |
| Water/sludge disposal | $0 | $4–$6 | −$5 |
| Downtime for consumable change | ~$1 | $8–$12 | −$9 |
| Total per 100 meters | $19–$27 | $57–$81 | −$38 to −$54 |
Ⅳ. The 5-Year TCO Ledger: Material Yield, Electricity, and Outsourcing Balance
1. The 8% raw material yield dividend: Tight kerf and common-line nesting
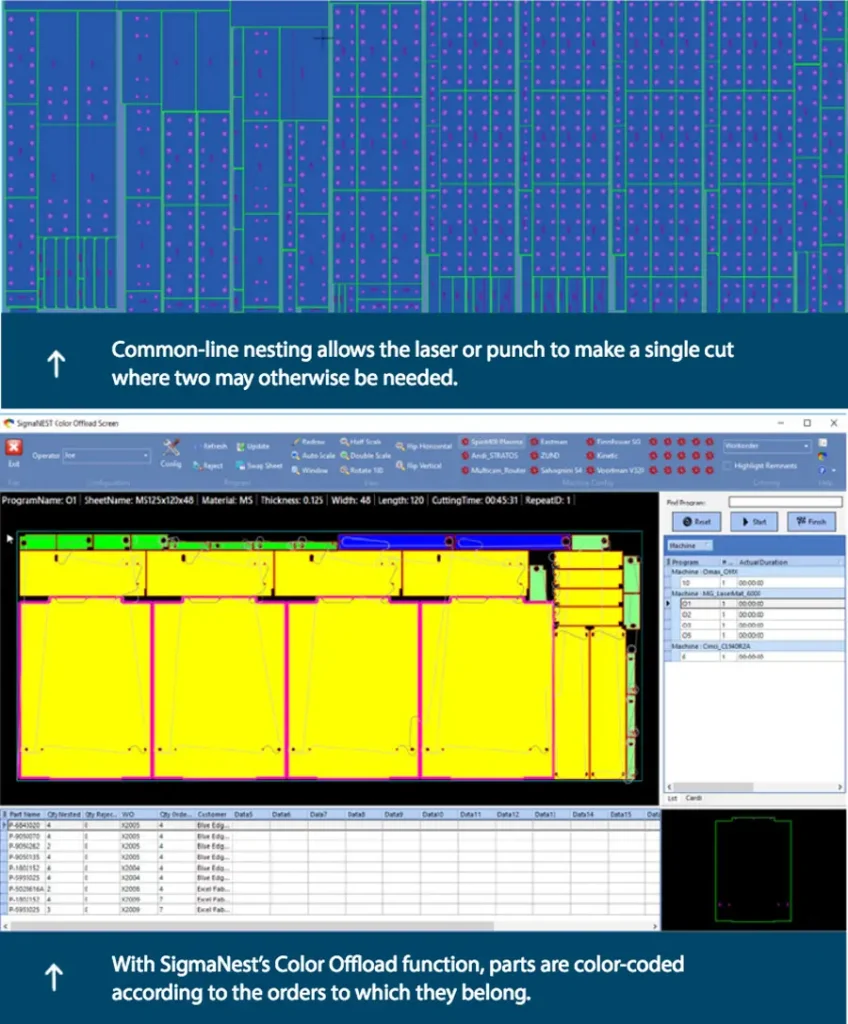
A fiber laser kerf of 0.4–0.6 mm on 16 mm plate is roughly one-sixth the width of a plasma kerf. The narrower cut allows tighter nesting: parts can be placed closer together, and common-line cutting (shared edges between adjacent parts) becomes practical.
On a 120-ton-per-month operation, the nesting yield improvement from 85% to 93% saves approximately 9.6 tons of steel per month. At $800/ton for structural plate, that is $7,680 per month, or $92,160 per year in raw material savings alone.
2. Secondary labor elimination ledger: Annual direct shop floor savings
The $59,904 annual deburring labor savings from Table 2 is a direct cash flow improvement. Add the handling and wheel wear savings, and the labor line alone returns roughly $68,000 per year.
This is the number that determines payback for most shops replacing a cnc plasma cutting table: not the machine price difference, but the annual cash that stops being spent on grinding labor and consumable churn.
3. Wall-plug efficiency and total lifecycle financial rollup
The fiber laser’s 35–40% wall-plug efficiency, compared to roughly 10% for a plasma power supply, reduces electrical consumption per part by 60–70%. On 4,000 annual operating hours, that difference is material.
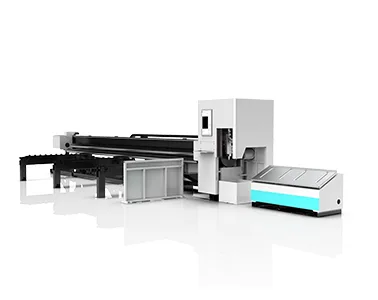
When all lines are rolled up—Capex, electricity, consumables, secondary labor, and material yield—the 5-year TCO advantage for a 12 kW fiber cell over a comparable cnc plasma cutting table is decisive. For fabricators running mixed plate and structural profile jobs, review the machine specifications of our heavy-duty 3kW–12kW plate and tube fiber laser cutting machine.
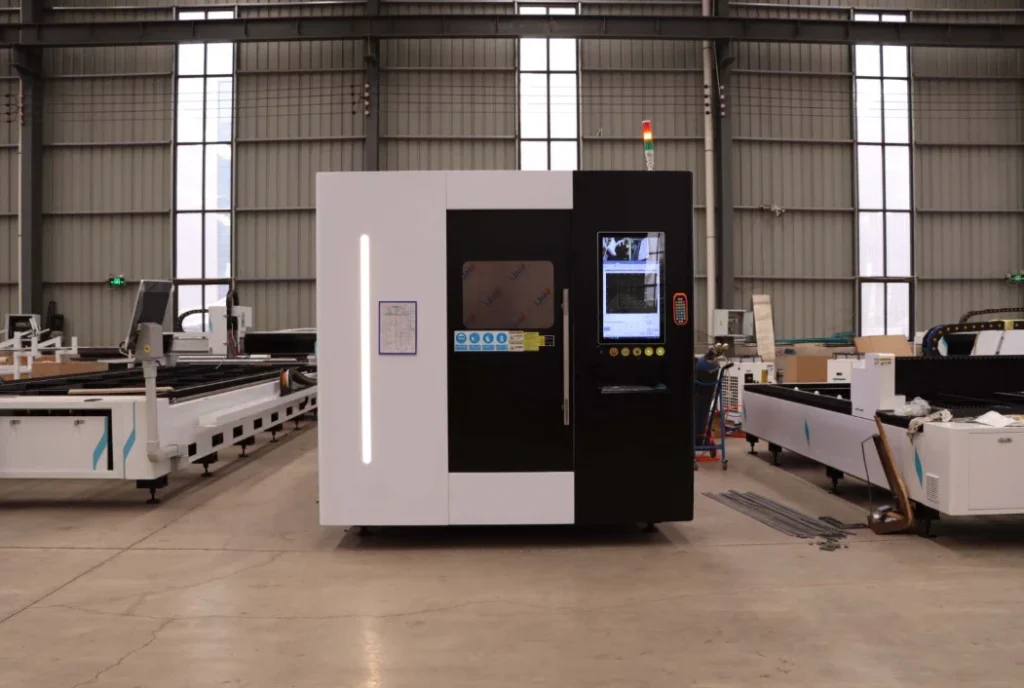
Table 4: 5-Year Total Cost of Ownership (TCO) Comparison: Laser vs. Plasma
| Cost Category | Fiber Laser (12 kW) | HD Plasma (200A) | 5-Year Delta |
| Initial capex | $280,000 | $130,000 | +$150,000 |
| Electricity (5 years) | $64,000 | $144,000 | −$80,000 |
| Consumables & spares (5 years) | $22,000 | $78,000 | −$56,000 |
| Secondary labor (5 years) | $23,000 | $323,000 | −$300,000 |
| Raw material waste (5 years) | $92,000 (93% yield) | $461,000 (85% yield) | −$369,000 |
| Water/sludge disposal (5 years) | $0 | $24,000 | −$24,000 |
| Residual value at 5 years | −$80,000 | −$20,000 | −$60,000 |
| Net 5-year TCO | ~$401,000 | ~$1,140,000 | −$739,000 |
Baseline: 120 tons/month of 16 mm structural steel, dual shift, $800/ton plate, $0.12/kWh electricity. TCO excludes tax incentives such as IRS Section 179, which further reduces the net cost of the fiber investment.
Ⅴ. Frequently Asked Questions
At what steel thickness does plasma still beat fiber laser?
Plasma retains an advantage above 25 mm, and on heavily rusted or scaled plate where laser requires slower pierce times. Below 20 mm, a 12–20 kW fiber laser is competitive on speed and superior on edge quality, consumables, and secondary labor elimination. At 16 mm, fiber is the clear choice.
How much labor does switching from plasma to laser save?
On a 120-ton-per-month structural operation, replacing a cnc plasma cutting table with fiber laser eliminates deburring and saves approximately 156 labor hours per month—roughly $60,000 per year in direct labor. Additional savings from handling, grinding wheel wear, and fit-up time push the total closer to $68,000 annually.
Can a fiber laser cut rusted or scaled plate like a plasma table?
Fiber lasers can cut rusted plate, but pierce time increases and cut quality may degrade on heavy scale. Plasma is more forgiving on heavily weathered material. For shops cutting a mix of clean and rusty plate, a fiber laser handles clean stock efficiently and rusty plate with adjusted pierce parameters.
مراجع
- ایزو ۹۰۱۳:۲۰۱۷ — قطع حرارتی — طبقهبندی قطعهای حرارتی, International Organization for Standardization
- ISO 8573-1:2010 — Compressed air — Contaminants and purity classes, International Organization for Standardization
- بخش 179 قانون مالیاتهای داخلی ایالات متحده — انتخاب تخصیص هزینه برخی داراییهای تجاری قابل استهلاک, سازمان خدمات درآمد داخلی
مطالعهٔ بیشتر
- In-House vs Outsourcing Laser Cutting: Payback Tipping Point — Break-even model for bringing plasma outsourced work in-house on a laser cell.
- 12kW Fiber Laser Cutting Machine Price & Factory Upgrade Guide — Capital budget and electrical infrastructure for the 12 kW class.
- Heavy Plate Laser Processing: Railway & Shipbuilding Standards — Geometry and tolerance requirements in heavy structural fabrication.
- Structural Steel Fabrication Laser ROI — Investment return model for structural steel shops moving to fiber.