A metal fabrication shop that produces flat blanks for automotive, appliance, or HVAC assembly faces a process decision that determines its cost structure for years: buy a stamping press with dedicated tooling, or install a laser blanking line that cuts blanks directly from coil.
The two processes are not interchangeable at every volume. Stamping wins on cycle time and per-piece cost at high volumes. Laser blanking wins on flexibility, tooling cost, and changeover speed. The decision hinges on the shop’s production profile — annual volume, part mix, and how often the design changes.
This guide compares the two processes on the four variables that determine the answer: tooling cost, changeover time, material utilization, and total production economics.
Ⅰ. The Stamping Baseline: Tooling Cost and Changeover Reality
1. The tooling cost structure
A stamping press does not produce a blank. It produces a blank through a die. The die is the production tool, and the die cost is the largest barrier to entry for any new part.
Two die types dominate blanking production. A blanking die cuts the outer profile of a flat part in a single press stroke. A progressive die performs multiple operations — cutting, piercing, notching — in sequence as the strip advances through the press. The progressive die is faster and handles more complex parts, but it costs more to build.
According to industrial tooling benchmarks from the Precision Metalforming Association and North American tooling survey data, dedicated blanking and progressive dies routinely cost between $50,000 and $150,000 per part variant. The lead time from die design to final tryout approval is 8 to 16 weeks.
2. The changeover cost
A stamping press is only as productive as its changeover speed. When the production schedule moves from one part to another, the die must be removed, the new die installed, and the press re-qualified. The changeover takes 30 to 120 minutes depending on the press size and the tooling complexity.
During the changeover, the press is not producing. On a high-volume line, the changeover time is a small fraction of the total operating time. On a mixed-production line with frequent changeovers, the downtime accumulates quickly.
3. Where stamping wins
Stamping is the low-cost process at high volume. When a single part runs for weeks or months without changeover, the die cost amortizes over hundreds of thousands of pieces, and the per-piece cost drops below any competing process. This is why automotive body panels and appliance housings are stamped, not laser cut.
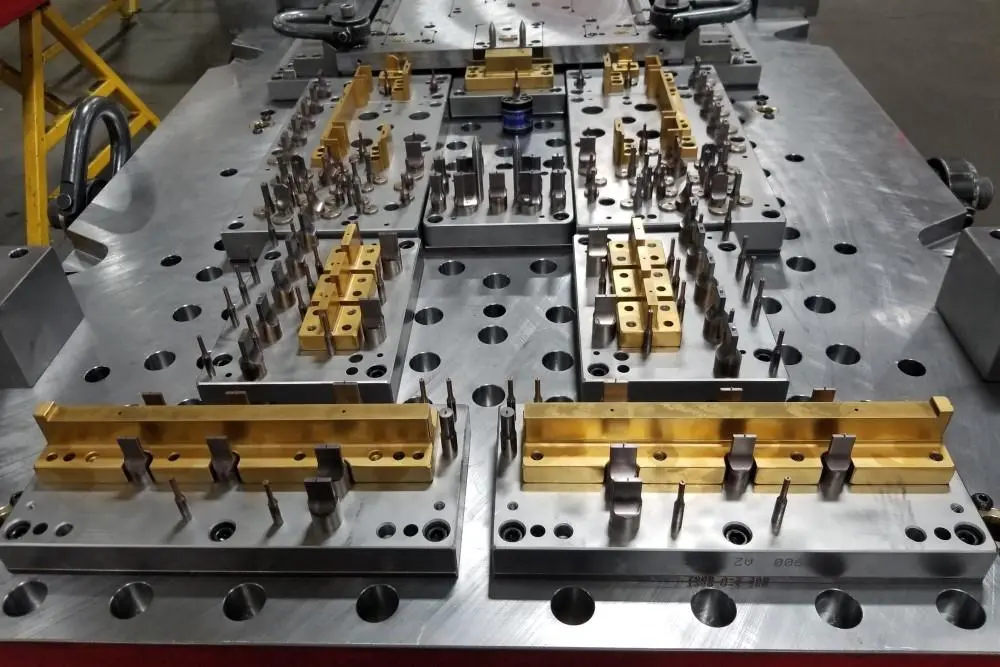
Table 1: Stamping vs Laser Blanking — Process Comparison
| 매개변수 | Traditional Stamping | Laser Blanking Line |
|---|---|---|
| Tooling required | Dedicated die per part | No tooling |
| Tooling cost | $50,000–$150,000 per variant | $0 |
| Tooling lead time | 8–16 weeks | 15 minutes (CAD to cut) |
| 전환 시간 | 30–120 minutes | 5–15 minutes |
| 자재 활용도 | 75%–82% | 93%–96% |
| Best volume range | > 50,000 parts/year | < 50,000 parts/year |
| Cycle time per blank | Seconds | Seconds to tens of seconds |
| Part design flexibility | Locked to die geometry | Unlimited |
Ⅱ. The Laser Blanking Line: Zero Tooling, CAD-to-Cut
1. How laser blanking works
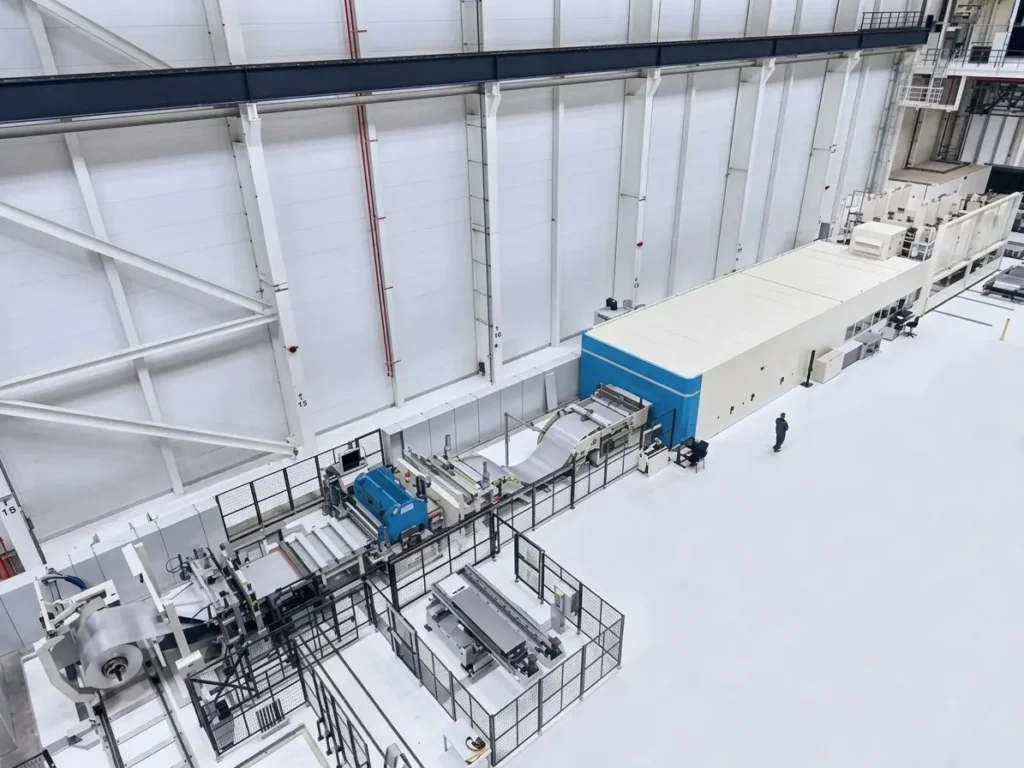
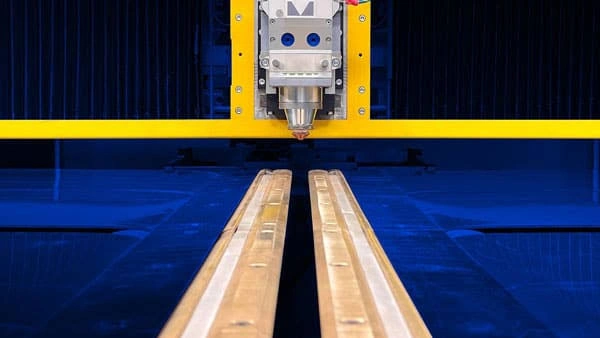
A laser blanking line processes metal coil directly. The coil is loaded onto a decoiler, fed through a precision leveler that removes coil set and cross-bow, and then advanced into a continuous laser cutting zone. The laser cuts the blank profile from the moving strip, and the finished blanks are sorted and stacked automatically.
The process does not use a die. The part geometry is defined in a CAD file, and the cutting path is generated by the nesting software. Changing from one part to another means loading a new program — not building a new tool.
2. The changeover advantage
The changeover on a laser blanking line is measured in minutes, not hours. When the production schedule changes, the operator loads the new program, verifies the material thickness and grade, and resumes cutting. The changeover takes 5 to 15 minutes, depending on whether the coil itself must be changed.
For a shop that produces 20 different part numbers per month, the cumulative changeover time saved is the single largest source of cost reduction. The same shop running a stamping press would spend 10 to 40 hours per month on die changes alone.
3. Material utilization
A laser blanking line uses the full coil width and cuts parts in a continuous strip. Adjacent parts share a common cut line, and there is no end-of-sheet waste because the strip has no end. The nesting yield on a well-designed laser blanking line reaches 93% to 96%, compared to 75% to 82% on a stamping press running a fixed die layout.
The material savings flow directly to the bottom line. On a shop processing 2,500 tons of steel per year, the 10 to 15 percentage point yield difference translates to 250 to 375 tons of additional usable material — a direct cash benefit that compounds with the steel price.
Ⅲ. The Footprint and Infrastructure Trade-Off
1. The laser blanking line footprint
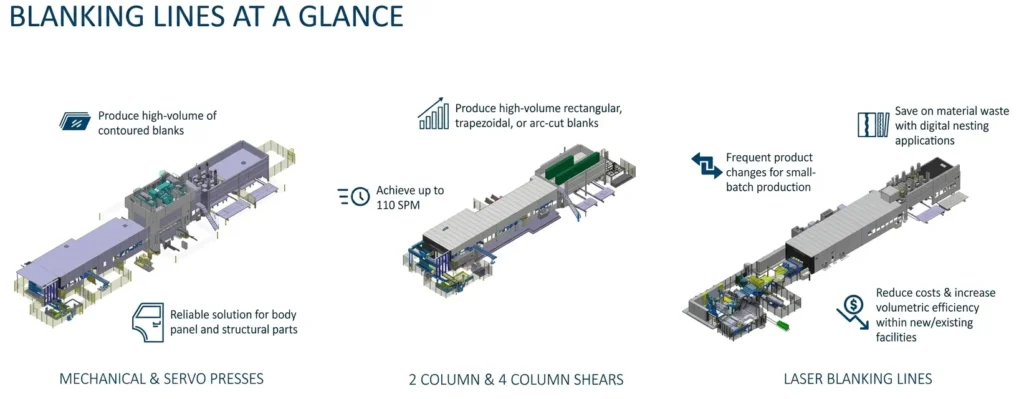
A continuous laser blanking line is a long machine. A standard 20-meter integrated line occupies approximately 130 square meters of floor space, including the decoiler, leveler, cutting zone, and stacking station.
The infrastructure requirements are equally demanding. The line needs a straight crane access route of at least 25 meters by 8 meters for coil loading. The floor must be rated for a 15-ton local static load at the coil position. The overhead crane must have a rated capacity of at least 10 tons to handle a full coil.
The full footprint and infrastructure breakdown is covered in our coil-fed laser line operational analysis.
2. The stamping press footprint
A stamping press occupies less floor space per unit of output than a laser blanking line. A typical 200-ton press with a progressive die occupies 30 to 50 square meters, including the die storage and changeover equipment.
But the stamping line requires additional space that is often overlooked. The die storage area for a shop running 20 part numbers occupies 50 to 100 square meters. The changeover equipment — die carts, cranes, and staging areas — adds more.
Table 2: Laser Blanking Line — Engineering Footprint
| 매개변수 | 사양 |
|---|---|
| Line length | ~20 m |
| 연면적 | ~130 m² |
| 기계 중량 | 15,000–18,000 kg |
| Crane access | 25m × 8m straight route |
| Floor load | 15 t local static load |
| Crane capacity | ≥ 10 t |
Ⅳ. Production Economics: When Each Process Wins
1. By annual volume
The decision is driven by volume. At annual volumes below 5,000 parts per variant, the stamping die cost cannot amortize, and laser blanking wins on total cost. Between 5,000 and 50,000 parts per variant, the decision depends on part complexity and changeover frequency. Above 50,000 parts per variant, the die cost amortizes to a few cents per part, and stamping wins on per-piece cost.
2. By part mix
A shop that produces 50 different part numbers per year cannot justify 50 dies. The tooling cost alone would exceed the cost of the laser blanking line. A shop that produces two part numbers at high volume should use stamping.
The decision is not binary. Many shops run both processes — stamping for the high-volume parts, laser blanking for the low-volume and prototype work.
3. By design change frequency
A product with a stable design that will not change for five years is a candidate for stamping. A product that is revised every six months, or a product family that expands with new variants, is a candidate for laser blanking. The cost of a design change on a stamping line is a new die — $50,000 to $150,000 and 8 to 16 weeks of lead time. The cost of a design change on a laser blanking line is a new CAD file.
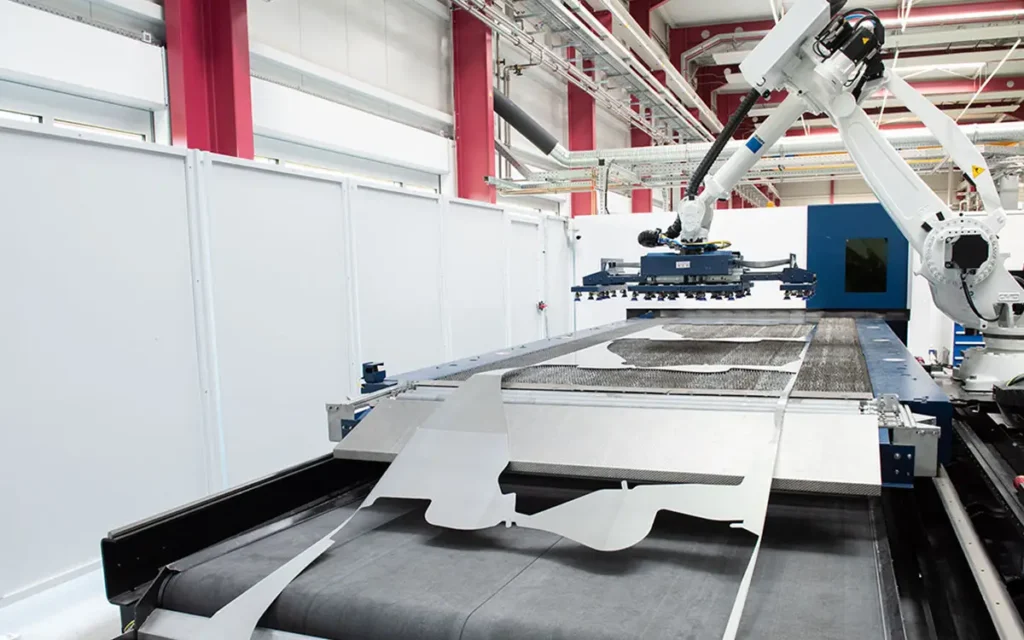
Table 3: Stamping Tooling Cost and Lead Time Reference
| Tooling Type | Typical Cost | 리드 타임 | Application |
|---|---|---|---|
| Blanking die | $50,000–$80,000 | 8–12 weeks | Simple outer profile |
| Progressive die | $80,000–$150,000 | 12–16 weeks | Complex multi-stage blanking |
Source: Precision Metalforming Association (PMA) tooling cost benchmarks, Harbour Results Inc. (HRI) North American tooling survey data.
Table 4: Volume-Based Process Selection
| 연간 발행 부수 | Recommended Process | Reason |
|---|---|---|
| < 5,000 parts | Laser blanking line | No tooling amortization needed |
| 5,000–50,000 parts | Depends on part mix | Evaluate changeover frequency |
| > 50,000 parts | Stamping | Tooling cost amortizes over volume |
Ⅴ. 자주 묻는 질문
Can a laser blanking line replace all stamping operations?
No. A laser blanking line cuts flat blanks. It does not perform forming, drawing, or three-dimensional shaping. Stamping processes that combine blanking with forming — such as progressive dies that produce a finished three-dimensional part — cannot be replaced by laser blanking. Laser blanking replaces the blanking step, not the forming step.
What is the typical die life and cost per part?
A progressive die for carbon steel blanking has a life of 500,000 to 2,000,000 strokes before refurbishment, depending on material thickness and die construction. At a cost of $100,000 and a life of 1,000,000 strokes, the tooling cost per part is $0.10. At 10,000 parts per year, the same die amortizes to $10.00 per part.
What is the minimum economic volume for a laser blanking line?
The break-even is approximately 5,000 parts per variant per year. Below that volume, the laser blanking line is the lower-cost process. Above it, the decision depends on part mix and changeover frequency. Shops with mixed production and frequent design changes benefit from laser blanking at higher volumes as well.
What training is required to operate a laser blanking line?
A laser blanking line requires an operator with experience in coil handling, laser cutting parameters, and nesting software. The training period is typically two to four weeks for an experienced laser operator. The skill set is different from a stamping press operator, who is trained in die setting and press operation.
Ⅵ. Commercial Verdict: Match the Process to the Production Profile
The laser blanking line is not a universal replacement for stamping. It is the correct process for a specific production profile: mixed part numbers, moderate volumes, frequent design changes, and a requirement for high material utilization.
A shop with a single high-volume part and a stable design should stay with stamping. A shop with 20 part numbers, changing designs, and a need to reduce material waste should evaluate laser blanking.
The two processes are not competing for the same work. They are complementary tools, and the shop that understands the boundary between them makes the right investment.
참고 문헌
- Precision Metalforming Association (PMA) — Tooling Cost Benchmarks, Precision Metalforming Association
- Harbour Results Inc. (HRI) — North American Tooling Survey, Harbour Results Inc.
- ISO 9013:2017 — 열절단 — 열절단 방식의 분류, 국제표준화기구
추가 자료
파이버 레이저 자금 조달: 2026년 장비 리스 대 구매 — 월별 납부 구조 및 제179조 적용.
Coil-Fed Laser Cutting vs. Sheet-Fed: Material Cost Delta, Nesting Yield & Payback Model — The material-form decision: coil vs sheet.
20kW 파이버 레이저 절단기: 비용 및 투자 수익률(ROI) 분석 — Capital payback and production throughput benchmarks for high-power laser blanking.
내부 수행 대 외주 레이저 절단: 비용 및 투자 수익률(ROI) — 자체 가공과 외주 가공 간의 손익분기점.