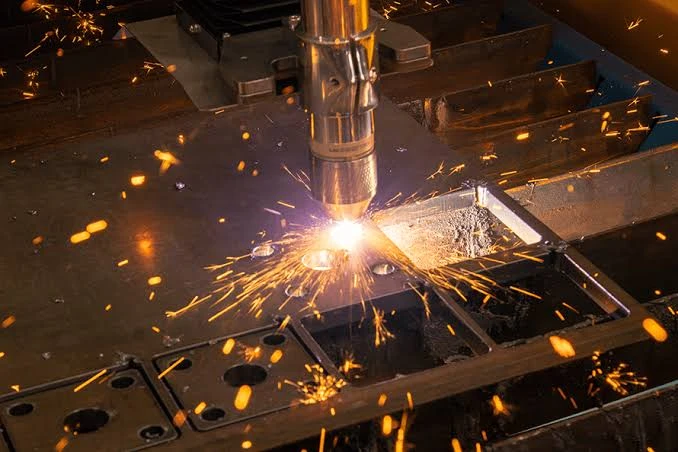
In modern structural steel fabrication, the bottleneck is rarely the cutting speed of the machine itself. The real constraint is the secondary handling: maneuvering heavy plates between the plasma table, the beveling machine, and the mag drill, then routing them to the welding bay. Every crane lift and every setup adds hidden labor costs and slows down the workshop flow.
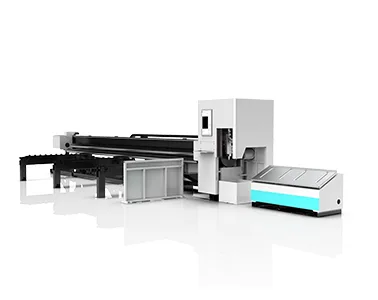
High-power fiber lasers equipped with 5-axis bevel heads eliminate these secondary steps. By cutting the profile, drilling bolt holes, and producing weld-ready bevels in a single pass, fabricators can compress their workshop footprint and reduce the cost per ton. This guide breaks down the economics of transitioning from traditional multi-step processing to integrated laser bevel cutting across commercial structural steel fabrication workflows.
1. The traditional material flow
In conventional structural steel fabrication plants, a heavy plate for a bridge girder or a commercial building column goes through at least three stations. First, a CNC plasma or oxy-fuel table cuts the outer profile. Second, the part is craned to a milling machine or a carbon arc gouging station to create the weld prep. Third, it moves to a radial drill press for the bolt holes.
This sequence introduces two major inefficiencies. First, the WIP (work-in-progress) inventory piles up, tying up working capital. Second, the crane and forklift traffic creates a severe bottleneck on the shop floor, decreasing the overall equipment effectiveness (OEE) of the entire facility.
2. The single-pass alternative
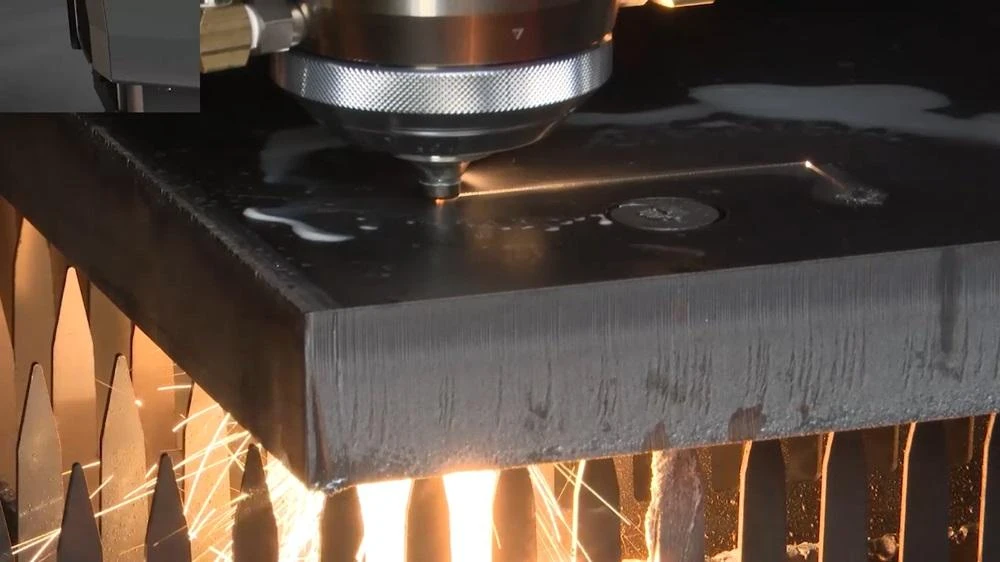
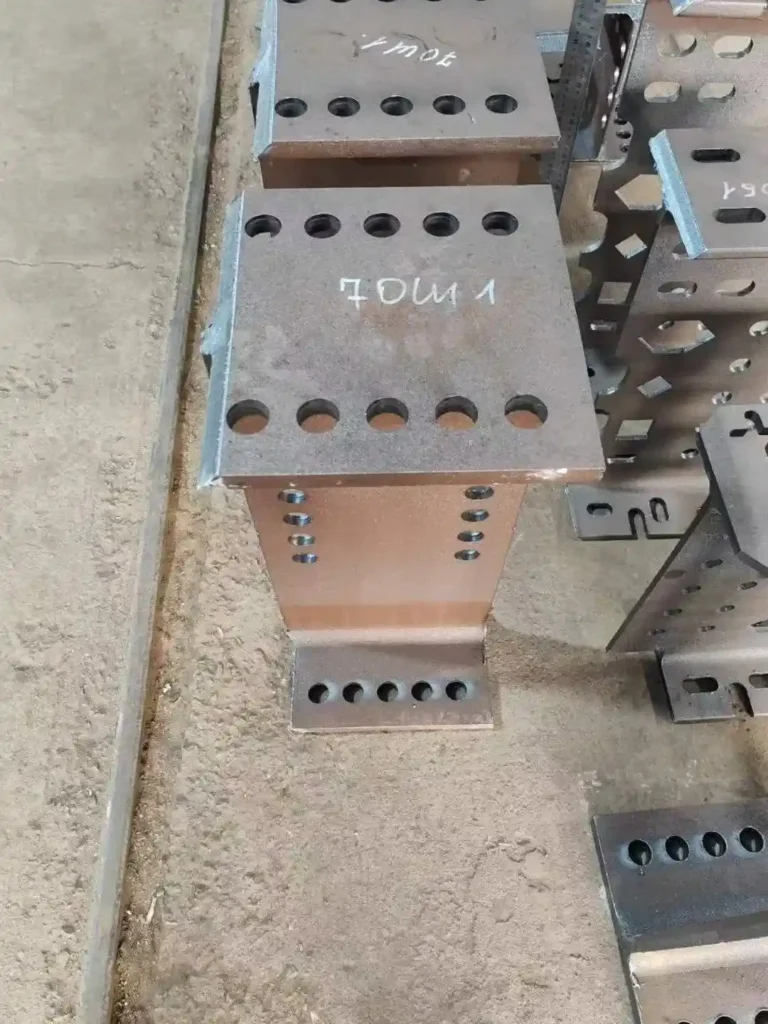
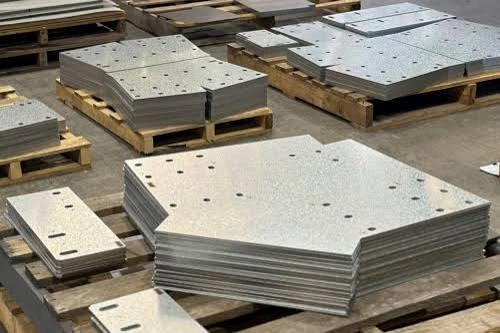
A 12kW to 20kW fiber laser system with a tilting bevel head cuts the outer geometry, pierces the bolt holes (achieving a 0.8:1 diameter-to-thickness ratio), and tilts up to ±45° to cut the V/Y/K weld prep simultaneously.
The result is a part that moves directly from the laser bed to the fit-up table. By consolidating operations within structural steel fabrication, the labor hours saved on manual grinding and secondary drilling drastically reduce the total cost per ton.
Ⅱ. Laser Bevel Cutting vs. Traditional Weld Prep
1. The physics of the laser bevel
When the cutting head tilts, the effective thickness of the material increases. At a 45° bevel, the beam must penetrate 1.41 times the nominal plate thickness. To maintain a clean cut, modern CNC systems use dynamic focus compensation, ensuring the beam waist remains optimized throughout the angled cut.
Unlike carbon arc gouging, which leaves a rough, oxidized surface that requires heavy grinding, a laser bevel produces a clean, scale-free edge that complies with ISO 9013 Range 2 and AWS D1.1 standards for high-tolerance structural steel fabrication.
Table 1: Traditional Weld Prep vs. 5-Axis Laser Beveling
| Parametre | Oxy-Fuel + Grinding | 5-Axis Fiber Laser Beveling | Avantaj |
| Bevel Method | Carbon arc gouging + manual grinding | Single-pass 5-axis dynamic cutting | Laser avoids secondary heat |
| Kenar Kalitesi | Rough, oxidized, requires cleanup | Clean, weld-ready | Eliminates grinding labor |
| Root Face Tolerance | ± 0.8 mm | ± 0.3 mm | Tighter weld gap control |
| AWS D1.1 Compliance | Requires manual prep | Achieved out-of-machine | Direct to fit-up |
| Process Speed | Slow, highly manual | Fast, fully automated | Higher throughput |
Ⅲ. The Economics of Laser Cutting Cost Per Ton
1. Consumables and gas
While the capital expenditure (Capex) of a high-power laser is higher than a plasma table, the operating expenditure (Opex) per ton is significantly lower when secondary operations are factored in.
A 20kW laser cutting 25mm carbon steel uses oxygen as the assist gas. The gas consumption is low, and the kerf is narrow, which means less material is wasted. More importantly, the elimination of milling tools, drill bits, and grinding discs shifts the variable costs from labor and consumables to electricity.
2. Labor and material utilization
Across high-tonnage structural steel fabrication, the most significant saving is labor. By eliminating the need to handle the part between multiple machines, a shop can reassign 2 to 3 operators to other tasks. Furthermore, laser-cut edges are perfectly square, which means the fit-up for welding is tighter, reducing the volume of weld wire required.
Table 2: Cost per Ton Breakdown (25mm Carbon Steel)
| Cost Category | Traditional (Plasma + Milling + Drill) | High-Power Laser (5-Axis Integrated) | Notes |
| Cutting / Processing Labor | $95 / ton | $40 / ton | 1 operator vs. 3-station handling |
| Gas & Power | $35 / ton | $25 / ton | Efficient kerf & oxygen cutting |
| Consumables (Tools, Discs) | $30 / ton | $8 / ton | No milling inserts or grinding discs |
| Secondary Grinding | $45 / ton | $0 / ton | Laser edge is weld-ready |
| Total Cost per Ton | $205 / ton | $73 / ton | 64% reduction in processing cost |
Ⅳ. Equipment Payback and Cash Flow
1. The Capex difference
A fully equipped 20kW fiber laser with a 5-axis bevel head costs significantly more than a standard high-definition plasma system. However, when calculating the ROI, the equipment cost must be weighed against the monthly savings in labor and secondary machine maintenance.
2. The payback calculation
For an enterprise scaling its structural steel fabrication output to 2,500 tons per year, the savings from reduced labor, zero grinding, and lower consumable costs create a massive cash flow surplus. The higher initial investment is typically amortized well within the equipment’s useful lifespan.
Table 3: Investment Payback Model (Annual Volume: 2,500 Tons)
| Financial Metric | Year 1 | Year 2 | Year 3 |
| Equipment Capex (15kW–20kW Bevel Laser) | -$350,000 | $0 | $0 |
| Annual Direct Labor Savings (2 Operators) | +$120,000 | +$126,000 | +$132,000 |
| Tooling & Grinding Consumables Saved | +$30,000 | +$34,000 | +$38,000 |
| Secondary Machine Maintenance Saved | +$25,000 | +$25,000 | +$25,000 |
| Annual Operating Savings (Opex Delta) | +$175,000 | +$185,000 | +$195,000 |
| Annual Net Cash Flow | -$175,000 | +$185,000 | +$195,000 |
| Cumulative Cash Position | -$175,000 | +$10,000 | +$205,000 |
| Payback Horizon | — | Breakeven at ~23.5 Months | High Cash Surplus |
Note: Calculations assume eliminating two full-time milling/drilling operators ($60,000/year fully burdened each). When factoring in U.S. IRS Section 179 first-year bonus depreciation, the net tax shield accelerates positive cash flow within 14 to 18 months.
Ⅴ. Facility Layout and Shop Floor Integration
1. Floor space savings
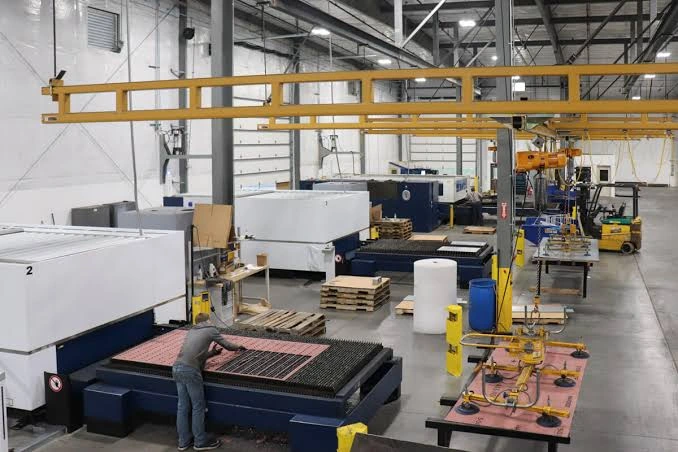
Eliminating the secondary milling and drilling stations frees up significant floor space. A typical beveling machine and radial drill require 50 to 80 square meters of dedicated floor space, plus the aisles required for forklift access.
The footprint of a large-format laser (such as a 6m × 2.5m bed) can be integrated into the existing workflow, but it does not require the additional 80 square meters of secondary equipment.
2. Power and utility configuration
Integrating a 20kW laser with a bevel head requires a robust power supply. The system, including the chiller and extraction, will draw close to 150 kVA. The facility must ensure the transformer capacity and voltage stability meet the machine’s demands.
3. Civil engineering and machine foundation parameters
High-acceleration gantries operating on heavy structural plates demand rigid foundations to avoid harmonic vibration. Fabricators evaluating large-format machinery can review the machine bed architecture and foundation vibration control
guide to prepare adequate shop floors[cite: 4].
Table 4: Workshop Space & Foundation Engineering Matrix (Structural Plate Tier)
| Equipment Platform | Certified Machine Model | Operating Footprint (m²) | Nominal Net Weight (kg) | Foundation Slab Requirement | Crane & Aisle Clearance |
| High-Precision Bevel Machine | YH6025AG | 32.53 m² | ~5,500 kg | 200–250mm reinforced concrete (C25/30) | >= 10-ton crane; 4.5m lateral access[cite: 4] |
| Dual Shuttle Table Laser | YH3015BD (Enclosed) | 30.45 m² | 4,391.01 kg | 200mm standard hardened concrete | Forklift aisle: 3.5m clearance[cite: 4] |
| Conventional Radial Drill Cell | Typical 2.5m Arm Drill | ~45.00 m² (with buffer) | ~3,200 kg | 150mm standard shop slab | Manual hoist; high scrap bin clutter |
| Dedicated Plate Edge Planer | 12m Mechanical Planer | ~85.00 m² (with rails) | ~8,000 kg | 300mm deep isolated trench | Overhead crane dedication required |
Ⅵ. Commercial Verdict: The Shift to Integrated Processing
The traditional multi-step workflow for structural steel fabrication relies on moving heavy parts between specialized machines. This model is capital-intensive in terms of floor space and labor.
High-power fiber lasers with 5-axis beveling consolidate this workflow. The ability to cut, drill, and bevel in a single setup drastically reduces the cost per ton. For contract facilities looking to scale their structural steel fabrication volume without expanding shop floor square footage, the integrated laser cell represents the most capital-efficient upgrade.
Frequently Asked Questions
Can a high-power fiber laser pierce code-compliant bolt holes in 25mm structural steel?
Yes. Modern 15kW and 20kW fiber lasers utilize frequency-modulated burst piercing to achieve a 0.8:1 diameter-to-thickness ratio. The resulting bolt holes feature a taper under 0.15mm, fully satisfying AISC and AWS D1.1 structural clearance tolerances without requiring secondary reaming.
What is the minimum monthly tonnage required to justify a 5-axis bevel laser?
A processing volume of 150 to 200 metric tons per month justifies the investment. At this scale, eliminating secondary radial drilling and bevel grinding recovers $14,000 to $22,000 monthly in skilled operator labor and consumables, achieving complete capital amortization in under 24 months.
How does compressed air assist gas purity affect thick plate cutting quality?
If utilizing high-pressure compressed air for structural steel, the air supply must strictly satisfy ISO 8573-1:2010 Class 1.2.2. Any trace residual oil or moisture will foul the cutting head protective window, destabilizing beam focus and creating severe dross adhesion.
Kaynakça
- ISO 9013:2017 Thermal Cutting Tolerances — Thermal cutting: Classification of thermal cuts, geometric product specification and quality tolerances. International Organization for Standardization.
- ISO 8573-1:2010 Compressed Air Contaminants & Purity Classes — Purity classes of compressed air with respect to particles, water, and oil. International Organization for Standardization.
- IRS Section 179 Capital Equipment Depreciation Guide — Internal Revenue Service Publication 946: How to depreciate commercial machinery and first-year expense deductions. Internal Revenue Servic.
Further Reading
Laser Cutter Cost Per Hour: The Full Operating Ledger: Calculate consumables, electricity, maintenance, and operator labor into an accurate hourly rate.
12kW Fiber Laser Cutting Machine Price & Upgrade Guide: Economic breakdown of stepping up to high-wattage cutting and evaluating transformer upgrades.
In-House vs Outsourcing Laser Cutting: Payback Tipping Point: Compare third-party fabrication costs against equipment financing to determine when purchasing a machine turns cash flow positive.
Laser Cutting Gas Cost: Compressed Air vs Liquid Nitrogen: Complete ledger on 16 Bar high-pressure shop air filtration to cut auxiliary gas expenditure by over 75%.