A 6kW fiber laser cutting machine carries a sticker price between $85,000 and $140,000. But the purchase order is not the cost. The cost is what the machine consumes every hour it runs. Laser cutter cost per hour answers a different question than machine price: not “what did I pay,” but “what does an hour of cutting actually cost me.” That number decides whether a job shop makes money or slowly bleeds it. So how much does it cost to run a laser cutter depends on six cost lines — power, assist gas, consumables, labor, depreciation, and downtime — and each one behaves differently as the machine scales from 3kW to 12kW.
Ⅰ. Why Machine Price Is Not the Answer
1. The Two Questions Buyers Confuse
A shop owner looking at a $120,000 fiber laser is asking a capital question. A shop owner calculating a job quote is asking an operating question. The first number is fixed and paid once. The second number repeats every cutting hour for the life of the machine. A machine can be cheap to buy and expensive to run. A machine can be expensive to buy and cheap to run. The only way to compare them is to build the hourly ledger.
2. What Goes Into One Cutting Hour
One cutting hour includes electricity, assist gas, nozzle and lens wear, operator time, a share of the machine’s capital cost, and a share of the maintenance reserve. Some of these scale with cutting time. Some are fixed monthly and depend on utilization rate. Mixing them up is the most common costing error in small fabrication shops.
Ⅱ. How Much Does It Cost to Run a Laser Cutter? The Six Cost Lines
1. Power
Power cost is the easiest to meter and the easiest to underestimate. A 6kW fiber laser draws roughly 18kW to 22kW at the wall during cutting, including the chiller, dust collector, and control cabinet. At $0.12 per kWh, that is $2.16 to $2.64 per cutting hour before any gas or consumables.
2. Assist Gas
Gas cost dominates thin-sheet cutting and disappears on thick-plate oxygen cutting. Nitrogen cutting on stainless steel at 14 bar can run $8 to $18 per hour depending on wall thickness. Compressed air retrofit can cut that to $1 to $3 per hour, which is why air payback is often measured in months, not years.
3. Consumables
Nozzles, protective lenses, and ceramic rings scale with cutting hours, not with capital cost. A shop running 160 cutting hours per month spends $160 to $480 monthly on consumables. The line item is small per hour but compounds across thousands of hours.
4. Labor
Operator cost per attended hour is the largest single line in most job shops that still run attended shifts. At a fully loaded $35 per hour and a one-operator-two-machine ratio, the effective labor cost per machine hour is $17.50. Lights-out automation is the only structure that reduces this line without reducing output.
5. Depreciation and Financing
A $120,000 machine financed over 60 months at 9% APR costs roughly $2,490 per month. Spread across 160 cutting hours, that is $15.56 per hour. Spread across 320 cutting hours, it drops to $7.78. Utilization rate is the dominant variable in this line, not the machine’s price.
6. Downtime and Maintenance Reserve
Unplanned downtime costs $75 to $120 per hour in lost profit. A single 8-hour downtime event erases $600 to $960 of margin. A maintenance reserve of $2 to $5 per operating hour is not optional — it is the cost of keeping the other five lines predictable.
Ⅲ. Power Consumption: The Cost You Can Meter
1. Wall-Plug Draw by Source Power
A 3kW source typically draws 10kW to 13kW at the wall. A 6kW source draws 18kW to 22kW. A 12kW source draws 32kW to 40kW. The ratio of cutting power to wall-plug draw is roughly 1:3 including chiller and dust collection. Quoting power cost from the source rating alone understates the real load by a factor of three.
2. Chiller, Dust Collector, Air Compressor
The chiller runs continuously during cutting. The dust collector runs whenever the cutting head is active. The air compressor runs whenever compressed air is used as assist gas. Together they add 6kW to 10kW to the wall-plug load on a 6kW machine — often more than the laser source itself.
3. kWh Rate and Utilization
Power cost is fixed per kWh but variable per cutting hour. A shop at $0.12 per kWh and 160 cutting hours per month pays the same monthly power bill whether the machine runs 160 hours or 300. The hourly rate falls as utilization rises. This is the same logic that applies to depreciation and financing.
Ⅳ. Assist Gas: The Cost You Can Cut
1. Nitrogen vs Oxygen vs Compressed Air
Nitrogen preserves the cut face on stainless steel but costs $8 to $18 per hour at 14 bar. Oxygen is cheaper per bottle on carbon steel but produces an oxidized edge. Compressed air sits between them on cost and quality, and pays back the compressor hardware in four to seven months.
2. Cost per Hour by Material and Thickness
The same gas at the same pressure costs different amounts per hour because cutting speed changes with thickness. Thin material cuts fast and consumes less gas per part. Thick material cuts slow and consumes more. The hourly gas cost is a function of pressure, nozzle size, and cutting speed.
3. When Air Pays Back the Compressor
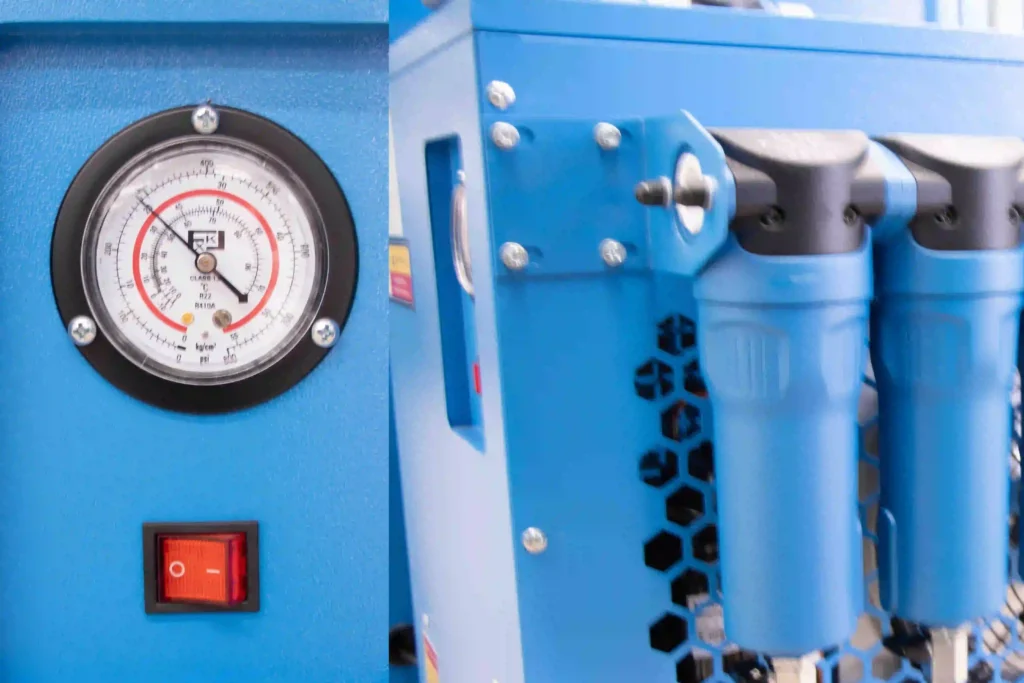
A screw compressor with dryer and five-stage filtration costs $8,000 to $15,000 installed. If nitrogen cost drops from $12 per hour to $2 per hour, the compressor pays back in 800 to 1,500 cutting hours — roughly six to twelve months at 160 hours per month.
Ⅴ. Consumables: The Cost That Scales with Cutting Hours
1. Nozzles, Lenses, Ceramic Rings
A nozzle lasts 200 to 800 cutting hours depending on material and pierce count. A protective lens lasts 400 to 1,200 hours. A ceramic ring lasts until impact. Each item is a small per-hour cost, but the sum is a real operating line.
2. Cost per Hour by Material Mix
Stainless and aluminum produce more dross and spatter, shortening nozzle and lens life. Carbon steel with oxygen cutting is gentler on consumables. A shop cutting mixed material should budget the higher end of the range.
3. Maintenance Reserve
The reserve covers chiller filters, deionized water, calibration, and unforeseen repairs. At $2 to $5 per cutting hour, the reserve is the cheapest insurance a shop can buy against a $15,000 chiller failure.
Ⅵ. Labor, Floor Space, and Overhead
1. Operator Cost per Attended Hour
A fully loaded operator cost of $35 per hour across a one-operator-two-machine ratio yields $17.50 per machine hour. A one-operator-one-machine ratio doubles it to $35. The manning ratio is a management decision, not a machine specification.
2. Lights-Out Share and Manning Ratio
Automation changes the labor line without changing the other five. A machine that runs unattended for four hours after an attended shift converts $17.50 per hour of labor into $0 per hour for those four hours. The machine cost is unchanged. The hourly rate falls.
3. Floor Space and Utilities
Floor space, lighting, and HVAC are overhead lines that are often ignored in hourly cost calculations. For a 6kW machine with automation, budget 120 to 200 square feet and $0.50 to $1.50 per square foot per month in utilities. This line rarely exceeds $1 per cutting hour but disappears if it is not tracked.
Ⅶ. Depreciation and Financing: The Cost You Already Committed
1. Straight-Line vs Section 179
Straight-line depreciation spreads the capital cost over five to seven years. Section 179 allows full deduction in the year of purchase, subject to income limits. The accounting treatment changes the tax bill, not the hourly cost. The hourly cost depends on the monthly payment and the utilization rate.
2. Lease vs Loan per Hour
A 60-month $1 buyout lease at $2,125 per month and a 60-month equipment finance agreement at $1,660 per month produce different hourly capital costs at the same utilization. The lease costs more per hour. The EFA costs less. The difference is the interest cost and the ownership structure.
3. How Utilization Changes the Hourly Rate
At 160 cutting hours per month, a $2,490 monthly payment is $15.56 per hour. At 320 cutting hours, it is $7.78. The same machine, the same payment, half the hourly cost. Utilization is the lever.
Table 1: Hourly Operating Cost by Source Power (160 Cutting Hours/Month, $0.12/kWh, 304 Stainless, Nitrogen)
| Cost Line | 3kW | 6kW | 12kW |
|---|---|---|---|
| Power (wall-plug) | $1.35/hr | $2.40/hr | $4.32/hr |
| Assist gas (N₂, 3mm 304) | $6.00/hr | $8.50/hr | $12.00/hr |
| Consumables | $1.50/hr | $2.00/hr | $3.00/hr |
| Labor (1 op / 2 machines) | $17.50/hr | $17.50/hr | $17.50/hr |
| Depreciation + financing | $9.40/hr | $15.56/hr | $24.90/hr |
| Maintenance reserve | $2.50/hr | $3.50/hr | $5.00/hr |
| Total hourly cost | $38.25/hr | $49.46/hr | $66.72/hr |
Ⅷ. The Full Ledger: 3kW vs 6kW vs 12kW
1. Hourly Cost Table by Power
The table above uses 160 cutting hours per month and nitrogen cutting on 3mm 304 stainless steel. Change any variable — gas, thickness, utilization — and the hourly rate changes. The table is a starting point, not a universal answer.
2. Break-Even Hours per Month
A job shop quoting a $75 per hour shop rate needs a machine hourly cost below $75 to make margin. At 160 cutting hours, all three power levels clear that bar. At 100 cutting hours, the 12kW machine’s depreciation line rises to $24.90 per hour and the total exceeds $70. Utilization is the deciding variable.
3. When the Machine Pays for Itself
A 6kW machine with a $2,490 monthly payment pays for itself when monthly net profit from the machine exceeds $2,490. At a $45 net margin per cutting hour, that is 56 cutting hours per month. Most job shops clear that bar in the first week of production.
Table 2: Break-Even Cutting Hours per Month by Power and Shop Rate
| Shop Rate | 3kW Break-Even Hours | 6kW Break-Even Hours | 12kW Break-Even Hours |
|---|---|---|---|
| $75/hr | 51 hrs | 66 hrs | 89 hrs |
| $100/hr | 38 hrs | 49 hrs | 67 hrs |
| $125/hr | 31 hrs | 40 hrs | 53 hrs |
| $150/hr | 26 hrs | 33 hrs | 44 hrs |
Table 3: Utilization Impact on 6kW Hourly Cost
| Cutting Hours/Month | Depreciation per Hour | Total Hourly Cost |
|---|---|---|
| 100 hrs | $24.90 | $58.80 |
| 160 hrs | $15.56 | $49.46 |
| 240 hrs | $10.38 | $44.28 |
| 320 hrs | $7.78 | $41.68 |
Table 4: Nitrogen vs Compressed Air vs Oxygen — Hourly Gas Cost (6kW, 3mm 304)
| Assist Gas | Pressure | Hourly Gas Cost | Cut Face Quality |
|---|---|---|---|
| Nitrogen (N₂) | 14 bar | $8.50 | Bright, oxide-free |
| Compressed air | 10 bar | $2.00 | Slight oxidation |
| Oxygen (O₂) | 0.6 bar | $0.80 | Oxidized edge |
Ⅸ. Frequently Asked Questions
How much does it cost to run a laser cutter per hour?
On a 6kW fiber laser cutting 3mm 304 stainless with nitrogen, the fully loaded hourly cost is approximately $49 per cutting hour at 160 hours per month. On a 3kW machine, the same job runs approximately $38 per hour. On a 12kW machine, approximately $67 per hour.
Is nitrogen or compressed air cheaper?
Compressed air is cheaper per cutting hour — approximately $2 versus $8.50 on a 6kW machine at 3mm 304. The trade-off is cut face quality. Compressed air leaves slight oxidation on stainless. For parts that will be painted or welded, the oxidation is acceptable. For visible stainless surfaces, nitrogen remains necessary.
What is the biggest hidden operating cost?
Downtime. An 8-hour unplanned stop costs $600 to $960 in lost profit — more than a month of consumables. The second biggest is underutilization, which raises the depreciation and financing line per hour without raising output.
How many hours per month to break even?
At a $100 per hour shop rate and a $49 per hour machine cost, the break-even point is roughly 49 cutting hours per month on a 6kW machine. Most job shops reach that in the first week of production. The real question is not break-even but the utilization rate above break-even.
Ⅹ. Conclusion
Laser cutter cost per hour is not one number. It is six cost lines, each with its own behavior as the machine scales from 3kW to 12kW. The capital price is fixed. The hourly cost is not. A shop that tracks the six lines — power, gas, consumables, labor, depreciation, and maintenance reserve — can quote jobs with margin instead of guessing. A shop that does not track them is quoting against a number that changes every month.
WSL Laser works with fabrication shops to model the full operating cost ledger against their actual part mix, material schedule, and utilization rate. If you want a side-by-side comparison of 3kW, 6kW, and 12kW machines against your own production data, bring your cutting schedule and material cost sheet. The math takes one call.
References
- SME — Laser Cutting Economics and Shop Rate Benchmarking, Society of Manufacturing Engineers, technical resources
- FMA — Operating Cost Benchmarks for Metal Fabrication, Fabricators & Manufacturers Association, technical resources
- ISO 9013:2017 — Thermal cutting — Classification of thermal cuts — Geometrical product specification and quality tolerances, ISO, 2017
- ELFA — Equipment Lease vs Buy Cost Analysis, Equipment Leasing & Finance Association, 2026
Further Reading
- Laser Cutting Business: Profit, Payback & Job Shop — How shop rate, utilization, and margin determine whether the machine pays for itself.
- Laser Cutting Quote: Price Per Meter & Part Cost Guide — The outbound quoting model that sits on top of the hourly cost ledger.
- Fiber Laser Cutting Machine Price: Cost & Value Guide — The capital cost side of the equation.
- Used Fiber Laser Cutting Machine: 2026 Guide vs New — When the secondhand market changes the hourly math.