A fabrication shop running standard flatbed equipment faces a critical capital decision when evaluating laser vs coil fed laser processing: does the raw material cost advantage actually justify the extra floor space, civil work, and machinery CapEx? The financial viability depends on annual tonnage throughput, and the break-even threshold is not the same for every facility.
This operational guide breaks down the core economics of an automated coil-fed laser cutting machine versus conventional sheet-fed cutting across four verifiable metrics: raw material price delta, continuous nesting yield, machine footprint constraints, and capital payback periods.
Ⅰ. Material Price Delta: Coil vs. Cut-to-Length Sheet
1. Where the price difference comes from
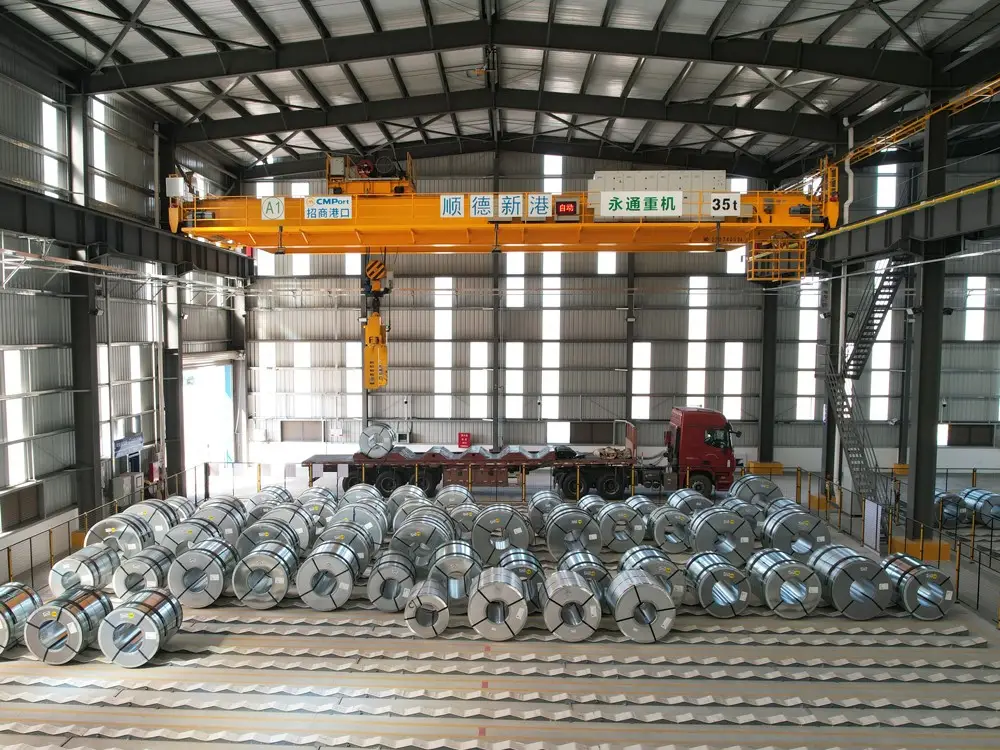
A steel mill sells master coil at the base price. Between the mill and the shop, a cut-to-length sheet passes through four additional cost layers: the service center’s leveling and shearing fee, the shearing tolerance loss at the edges, the secondary warehouse handling, and the second-leg truck freight.
None of those four layers exist when the shop buys the master coil directly. That is the entire source of the price delta.
2. The delta across three material types
The delta is not the same for every steel grade. Carbon steel carries a proportionally larger processing markup than stainless, because the stainless base price is already high.
Table 1: Coil vs. Cut-to-Length Sheet Price Delta Matrix
| Chất liệu | Coil Base Price | Cut-to-Length Premium | Delta as % of Coil Price | Ghi chú |
|---|---|---|---|---|
| Cold-rolled carbon steel (CRC) | Benchmark | +$80–$140/ton | 12%–18% | Largest relative delta |
| Galvanized steel (GI) | Benchmark | +$90–$150/ton | 12%–17% | Higher processing fee |
| Stainless 304 | Benchmark | +$150–$250/ton | 8%–12% | High base price dilutes % |
Data benchmarked against long-term historical spot price indices (e.g., S&P Global Platts, Fastmarkets) for master coil vs. toll-processed sheet.
3. Annual cash impact by tonnage
At 1,000 tons per year, the material delta alone is $80,000–$140,000. At 2,500 tons, it is $200,000–$350,000. At 5,000 tons, it is $400,000–$700,000. That cash flow appears in the first year of coil operation, before any productivity gain.
Ⅱ. Continuous Nesting vs. Static Sheet: The Geometry of Yield
1. Why sheet nesting wastes material at the edges
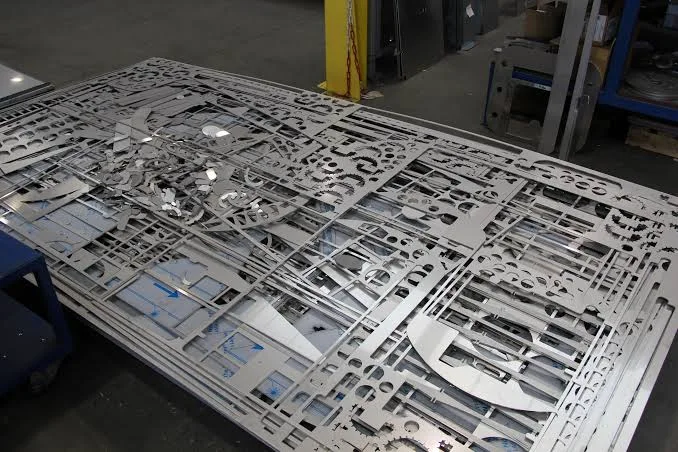
A standard 1,500 × 3,000mm sheet has a clamping margin of 15–20mm on all four edges. That margin exists because the cutting head needs clearance to accelerate and decelerate, and the sheet needs to be held in position. The margin is scrapped material.
The sheet also has a fixed end-of-sheet waste zone. When the nest reaches the trailing edge, the remaining strip is too short to fit another part, and it becomes scrap.
2. How coil eliminates both
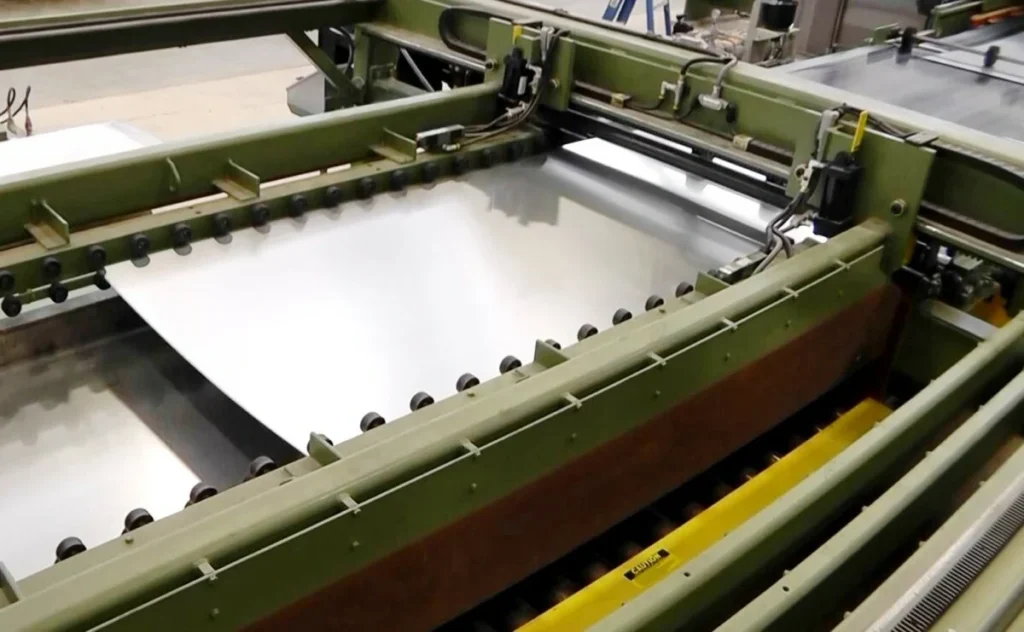
Coil-fed cutting uses a continuous strip. The strip is fed through the cutting zone without a trailing edge, so there is no end-of-sheet waste. Adjacent parts can share a common cut line, eliminating the web of material between them.
The result is a nesting yield that is 8–12 percentage points higher than discrete sheet nesting.
3. The nesting yield formula
The yield is calculated as the ratio of total part area to total material area consumed:
η_nest = [ Σ(A_i × n_i) / (W_coil × L_feed) ] × 100%
Where:
- A_i = area of individual part
- n_i = quantity of that part
- W_coil = coil width
- L_feed = feed length consumed
4. Typical yield comparison
On a mixed-part nest with an average part size of 300–600mm, sheet-fed cutting yields 82%–86%. Coil-fed continuous nesting yields 93%–96%. The gain is largest for small parts, because the end-of-sheet waste represents a larger fraction of the material consumed.
Ⅲ. Full Process Cost Comparison
1. The cost structure beyond material
Material cost is the largest line item, but it is not the only one. The full comparison includes material utilization, loading labor, changeover downtime, floor space, and infrastructure.
Table 2: Coil-Fed vs. Sheet-Fed Full Process Cost Comparison
| Cost Dimension | Sheet-Fed Line | Coil-Fed Line | Source of Difference |
|---|---|---|---|
| Raw material purchase | Cut-to-length retail | Master coil mill price | $80–$140/ton |
| Material utilization | 82%–86% | 93%–96% | Continuous nesting |
| Loading labor | Per-sheet crane lift | Continuous coil feed | Fewer changeovers |
| Changeover downtime | 8–15 min per sheet | 20–30 min per coil | 20+ daily changeovers reduced to 1–2 |
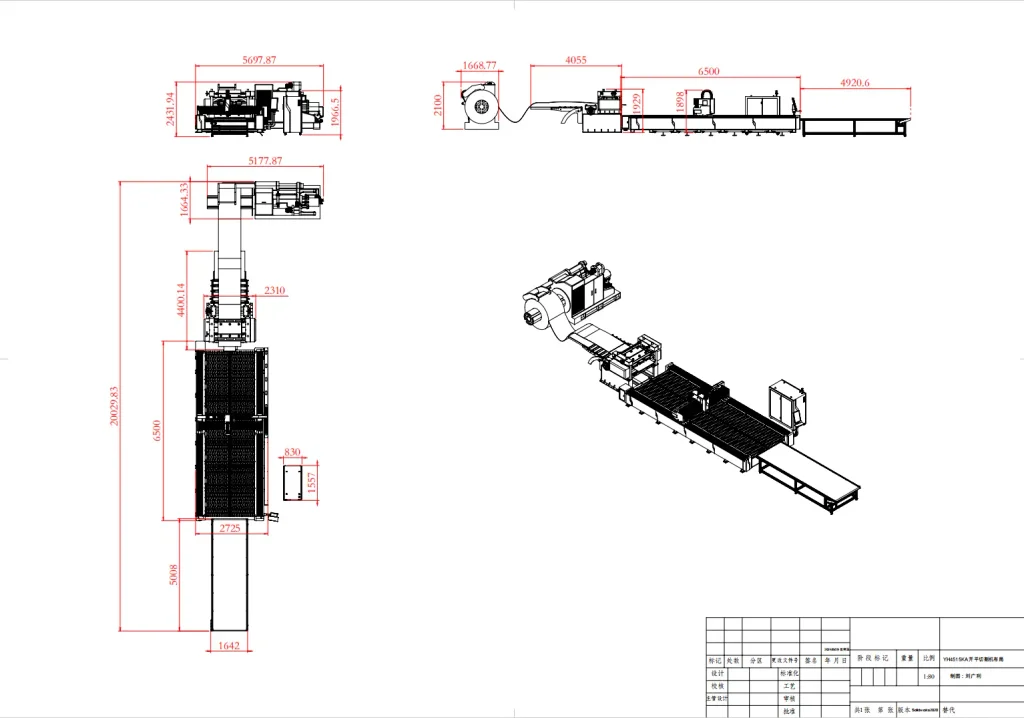
| Floor space | 30.45 m² (WSL-Pro 3015) | 130.19 m² (WSL-CL4515) | 4.28× footprint |
| Foundation | Standard 150mm slab | Reinforced pad + 10t crane | Hidden capex |
2. The effect of changeover downtime on OEE
A sheet-fed shop changes material 20 or more times per day. Each changeover stops the machine for 8–15 minutes. The cumulative downtime is 3–5 hours per day.
A coil-fed line changes material once or twice per day. The cumulative downtime is 30–60 minutes. The OEE difference is 15–25 percentage points, which flows directly into the shop’s effective capacity.
Ⅳ. Payback Model Across Three Production Volumes
1. The variables
- T = annual steel tonnage processed (tons/year)
- ΔP_material = material purchase saving per ton ($/ton)
- ΔY_yield = yield improvement saving per ton ($/ton)
- ΔC_capex = equipment capex difference ($)
- ΔC_infra = infrastructure retrofit capex ($)
- ΔC_labor = annual labor saving ($/year)
2. The payback formula
Simple Payback (years) = (ΔC_capex + ΔC_infra) / [ (ΔP_material + ΔY_yield) × T + ΔC_labor ]
The numerator is the one-time investment. The denominator is the annual cash benefit. The result is the number of years required to recover the investment.
3. Three production scenarios
Table 3: Payback Model Across Three Annual Tonnages
| Annual Volume | Material Saving | Nesting Saving | Labor Saving | Annual Net Benefit | Capex Delta | Static Payback |
|---|---|---|---|---|---|---|
| 1,000 t | $80,000–$140,000 | $50,000–$80,000 | $25,000 | $155,000–$245,000 | $250,000–$350,000 | 12.2–27.1 months |
| 2,500 t | $200,000–$350,000 | $125,000–$200,000 | $45,000 | $370,000–$595,000 | $250,000–$350,000 | 5.0–11.4 months |
| 5,000 t | $400,000–$700,000 | $250,000–$400,000 | $70,000 | $720,000–$1,170,000 | $250,000–$350,000 | 2.6–5.8 months |
Capex delta is an industry equipment benchmark for integrated decoiling-leveling continuous laser blanking lines. Payback excludes Section 179 tax treatment.
4. The break-even line
At 1,000 tons per year, the payback can extend beyond 24 months. The coil line is not the right investment at that volume. At 2,500 tons, the payback is inside 12 months, and the coil line becomes the default choice. At 5,000 tons, the payback is inside 6 months and the question is not whether to invest but how quickly the line can be installed.
Ⅴ. Procurement Decision Checklist
1. Coil weight and decoiler matching
The decoiler must be rated for the coil weight the shop will purchase. Coils are supplied in 5, 10, and 15-ton ranges. The decoiler’s mandrel capacity and the coil’s inner diameter must be verified before purchase.
2. Material specification switching
The line must be able to switch between steel grades and thicknesses without excessive downtime. Carbon steel, galvanized, and stainless each have different surface requirements. Cross-contamination between grades is a quality risk, and the changeover procedure must include cleaning.
3. Leveling quality and thickness tolerance
The leveler must produce a flat strip that the cutting head can follow at a consistent standoff. If the strip has residual coil set, the cutting head must compensate dynamically, and cut quality degrades. The leveler’s roll count and flatness specification determine whether this is an issue.
Ⅵ. Hard Shop Floor Requirements and Hidden Capex
1. The floor space requirement is not negotiable
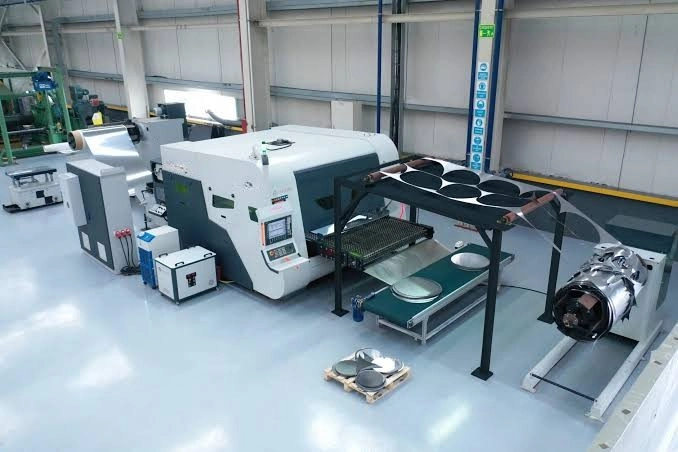
The comparison below uses verified machine engineering dimensions rather than speculative ranges. The sheet-fed baseline is the WSL-Pro 3015 enclosed exchange-table system. The continuous reference is the WSL-CL4515 coil-fed laser cutting machine, an integrated automated line featuring uncoiling, multi-roll precision leveling, continuous laser blanking, and automated parts sorting.
Table 4: Footprint and Infrastructure Comparison
| Tham số | WSL-Pro 3015 Sheet-Fed Exchange Table | WSL-CL4515 Coil-Fed Line |
|---|---|---|
| External dimensions (L × W) | 8.80m × 3.46m | 20.03m × 6.50m |
| Floor area | 30.45 m² | 130.19 m² |
| Machine weight | 4,391 kg | 15,000–18,000 kg (config-dependent) |
| Required aisle clearance | Standard shop aisle | 25m × 8m straight crane access |
| Floor load requirement | Standard 150mm reinforced slab | Reinforced pad + 15t local static load per coil |
| Crane requirement | Standard shop crane | ≥ 10t rated lifting capacity |
WSL-CL4515 weight is a baseline integrated value, varying with decoiler tonnage capacity and leveler roll configuration.
2. The hidden capex behind the line
The machine purchase price is not the full investment. The infrastructure retrofit adds cost that is often left out of the initial budget:
Table 5: Infrastructure Retrofit Capex Estimate
| Retrofit Item | Estimated Cost | Ghi chú |
|---|---|---|
| Foundation reinforcement | $15,000–$40,000 | For 15t local static load |
| Crane upgrade or installation | $25,000–$60,000 | ≥ 10t rated capacity |
| Electrical capacity upgrade | $5,000–$15,000 | Higher power draw |
| Aisle modification or layout change | $10,000–$30,000 | 25m × 8m straight access |
Estimated civil and mechanical infrastructure retrofitting costs based on typical North American/European industrial job shop standards.
3. When not to buy a coil-fed line
A coil-fed line is the wrong investment if any of the following is true:
- Annual tonnage is below 1,000 tons
- The shop does not have a 25m × 8m straight crane access route
- The floor cannot support a 15-ton local static load
- The shop does not have a crane rated at 10 tons or higher
- The product mix is high-variety, low-volume with frequent material changes
If any of these conditions applies, the material saving cannot be realized, and the investment does not pay back.
Ⅶ. Commercial Decision Framework
1. By annual tonnage
| Annual Tonnage | Recommended Approach |
|---|---|
| Under 1,000 t | Sheet-fed laser with higher power or automation |
| 1,000–2,500 t | Hybrid: sheet-fed plus coil-fed for high-volume parts |
| Over 2,500 t | Coil-fed line as primary production method |
2. By order profile
A shop with many part numbers and low volume per part should stay sheet-fed. The changeover cost between coil grades exceeds the material saving. A shop with few part numbers and high volume per part should move to coil. The material saving and the changeover reduction both apply.
3. By growth trajectory
A shop planning to double production within three years should design the coil line into its facility plan now, even if the installation is deferred. The infrastructure requirements — foundation, crane, aisle — cannot be added later without significant disruption.
Ⅷ. Finance FAQ
Q1: At 1,500 tons per year, is sheet-fed or coil-fed the better investment?
At 1,500 tons, the payback on a coil line is roughly 8–18 months, depending on the material mix and the actual capex. The decision hinges on whether the shop can fill the line’s capacity in the next three years. If the volume is stable, sheet-fed is the lower-risk choice. If the volume is growing, coil-fed pays back faster.
Q2: Does the material price advantage get offset by the higher equipment depreciation?
The material price advantage is an operating cash benefit that appears in the first year. The depreciation is a non-cash accounting charge spread over the asset life. The cash payback calculation uses the material saving, not the depreciation. The accounting treatment affects reported earnings, not the cash payback.
Q3: If the shop does not have 25m × 8m of straight crane access, is there a compromise?
No. A coil line requires the full straight access for coil loading. A curved or obstructed path prevents safe coil handling. The shop can either reconfigure the layout or select a sheet-fed solution. There is no partial coil line that avoids this requirement.
Q4: What minimum order quantity does the steel supplier require for coil?
Most steel service centers require a minimum order of one full coil per grade and thickness. A coil typically weighs 5–15 tons. A shop that cannot commit to that volume per order should buy cut-to-length sheet.
Technical Summary
A coil-fed laser cutting line is not a faster sheet-fed laser. It is a different material procurement model and a different production flow. The material price delta, the nesting yield gain, and the changeover reduction are real and quantifiable. The floor space requirement and the infrastructure retrofit are also real, and they are frequently underestimated.
The decision is not which technology is better. The decision is whether the shop’s annual tonnage justifies the investment, and whether the facility can support the line. Both questions must be answered yes before the purchase makes sense.
Tài liệu tham khảo
- ISO 9013:2017 — Thermal cutting — Classification of thermal cuts, International Organization for Standardization
- ASTM A1008/A1008M — Standard Specification for Steel, Sheet, Cold-Rolled, Carbon, Structural, High-Strength Low-Alloy, ASTM International
- Điều 179 của Luật Thuế Thu nhập Liên bang (IRS) — Lựa chọn hạch toán vào chi phí một số tài sản kinh doanh có thể khấu hao, Cục Thuế Liên bang
Tài liệu tham khảo thêm
- 20kW Fiber Laser Cutting Machine: Cost & ROI Analysis — Capital payback and production throughput benchmarks for heavy plate cutting.
- Tube Laser Cutting Machine: Zero-Tailing Chuck ROI & Scrap Reduction — Material recovery mechanics and remnant reduction on the tube side.
- In-House vs Outsourcing Laser Cutting: Cost & ROI — The financial break-even between purchasing machinery and subcontracting.
- Tài chính cho máy laser sợi quang: So sánh giữa thuê và mua thiết bị vào năm 2026 — Monthly capital allocation structures and IRS Section 179 tax treatment.